How to shorten injection moulding cycle time without losing quality? Start with cooling

In plastics processing, seconds decide the result. Talk about efficiency usually centres on injection speed or automated part removal, yet most of the time goes to cooling: the literature puts it at up to 80% of the cycle.
Below: how to shorten that stage so that the gain in OEE is real and does not come back as a customer complaint.
Why a few seconds make a big difference
Within a cycle, injection with holding pressure, and then mould opening, ejection and closing, are short. For the rest of the time the machine waits until the plastic in the cavity gives up its heat and the part is stiff enough to be removed safely.
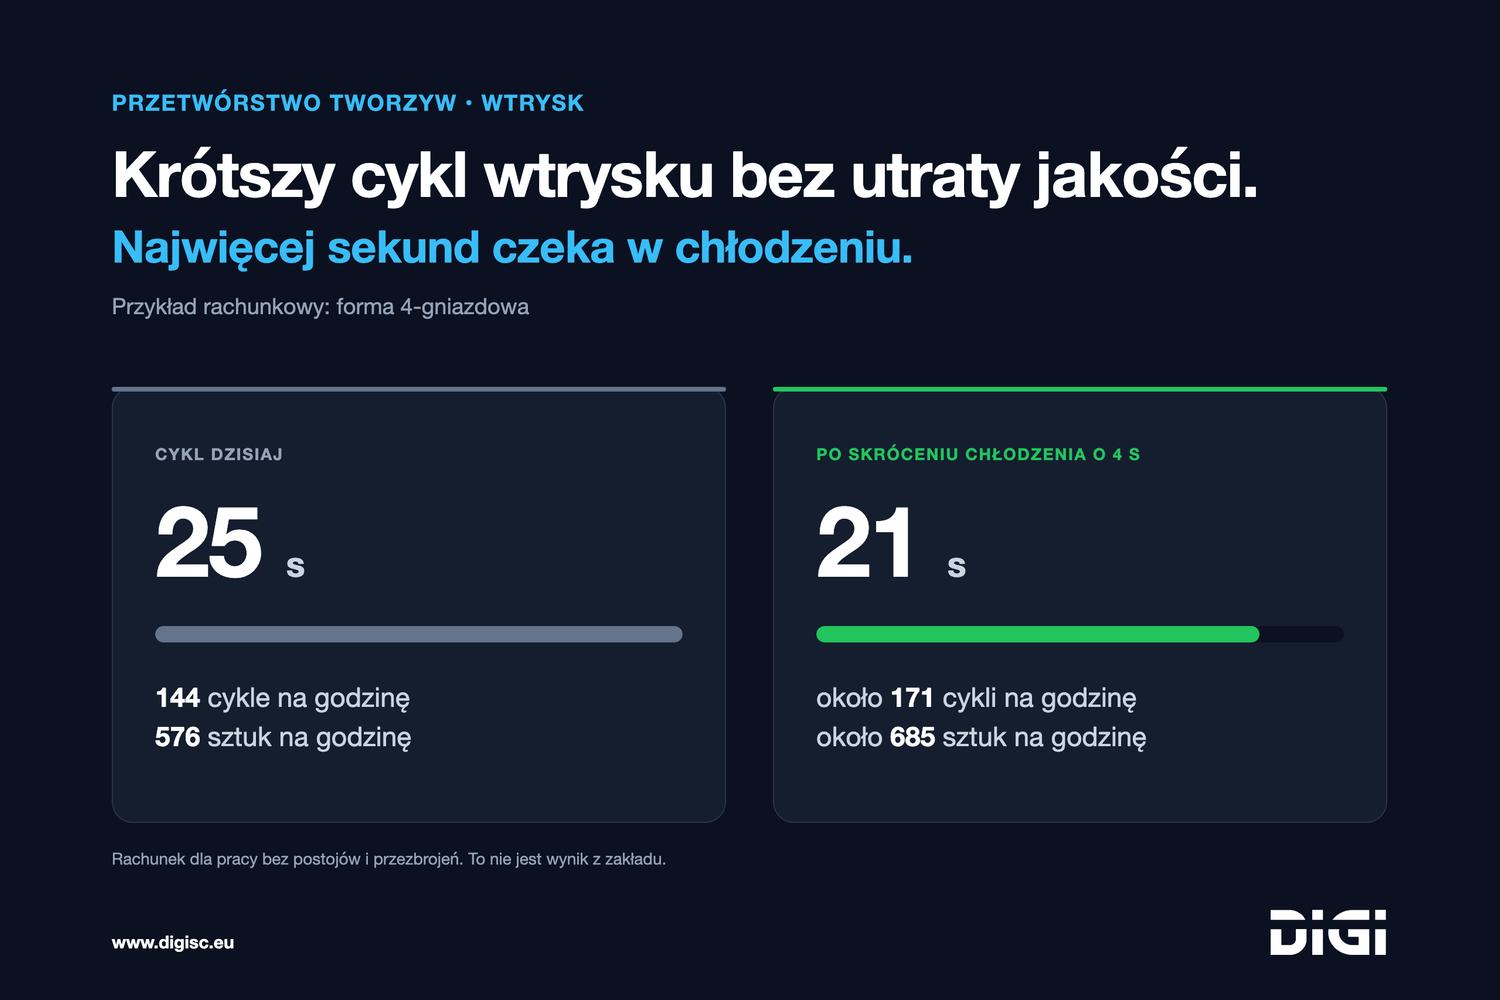
Let us run the numbers for a 4-cavity mould.
25 s cycle: 3600 / 25 = 144 cycles/h × 4 cavities = 576 parts/h
21 s cycle: 3600 / 21 ≈ 171 cycles/h × 4 cavities ≈ 685 parts/h
If better cooling takes 4 seconds off, which is 16%, an eight-hour shift yields about 880 more parts, and three shifts for 250 days a year about 658 thousand parts from the same machine.
This calculation assumes no stops and no changeovers, so it shows the upper limit. In a real plant the gain shrinks by however long the machine stands still.
Shorter cooling versus quality control
When pressure on the part price grows, the easiest thing to do is to shave 2 or 3 seconds of cooling off at the machine controller. Performance in OEE (Overall Equipment Effectiveness) goes up at once and the reports turn green. The problem shows up several hours later in quality control or, worse, on the customer’s assembly line.
What happens to a part that leaves the mould too hot?
- Post-mould shrinkage and warpage. Plastic that has not cooled below its heat deflection temperature (HDT) keeps moving outside the mould. This applies above all to semi-crystalline materials (PA, POM, PP, PBT), in which crystallisation continues after the mould opens. The part bends, loses flatness and goes out of tolerance.
- Ejector marks. A part that is too soft gets dented locally as it is pushed out of the mould.
- OEE that only looks high. A faster cycle raises performance, but every rejected part lowers quality, the third component of OEE. Manual sorting and complaints cost extra, and the indicator does not show them.
Five ways to shorten cooling and keep the dimensions
Cutting the time on the clock is not enough. The mould has to remove heat faster and more evenly.
1. Turbulent flow, not just a low temperature
A common reflex is to lower the temperature on the temperature controller, for example from 40°C to 20°C. The effect is often weaker than expected: colder water is more viscous, so at the same flow rate turbulent flow is harder to reach.
Heat removal depends on exactly that, turbulent flow. Flow is considered fully turbulent at a Reynolds number above 4000. In laminar flow the water in the middle of the channel removes hardly any heat, and an insulating layer forms at the walls. A higher flow rate (l/min), which means the right pump and connector cross-sections, often does more than lowering the water temperature.
2. Places where heat builds up
Cycle time is set by the hottest point of the part. These are usually thick walls, junctions, deep ribs or narrow cores that drilled channels can hardly reach.
Inserts made of high-conductivity alloys help, for example beryllium copper or copper alloys such as Ampcoloy, which conduct heat several times better than tool steel. More demanding projects use conformal cooling: metal 3D-printed inserts whose channels follow the shape of the part. The gain depends on the part and varies widely across published studies.
3. Clean cooling channels
Limescale, rust and biological deposits in the mould channels insulate the steel from the water. Limescale conducts heat many times worse than steel, so a layer of around a millimetre already lowers cooling efficiency noticeably.
Flushing the cooling system regularly with descaling agents, ideally after every larger production run and as part of planned mould maintenance (TPM), keeps heat removal at the level of a new mould.
4. Holding time set by a gate freeze test
Holding pressure is often applied longer than needed. Once the gate has frozen, further holding no longer changes the weight or the dimensions of the part. It only lengthens the cycle and adds residual stress around the gate.
A simple test is enough: weigh the parts while extending the holding time step by step. The point at which the weight stops rising gives the holding time you need.
5. Cooling outside the mould
With very thick-walled parts, for example in PE or PP, waiting in the mould for the whole cross-section to cool does not pay off. If the part is already stiff enough on the outside to be removed without deforming, the rest of the cooling can move outside the machine. A robot places the part in a cooling station (an air tunnel or a water bath) while the machine starts the next cycle.
Change the cycle on data, not on a hunch
Cycle time changes are best run the way Scientific Molding teaches: on measurements, not on intuition. Three things help.
- Flow and temperature difference on every circuit. Electronic flow meters with logging, instead of manual readings, show the flow rate (l/min) and the water temperature difference between the inlet and outlet of a circuit. A channel that is clogging up then shows before the defective parts do.
- A batch linked to the conditions it was made in. If you know which pallets left the machine before the settings changed and which after, a complaint can be narrowed down to specific batches.
- Thermal imaging right after the mould opens. The camera shows uneven temperature distribution on the part surface. Compare that picture with measurements on a coordinate measuring machine (CMM) taken once the part has stabilised.
What DiGi shows of this
DiGi does not measure flow or temperatures in the mould circuits. It shows the effect of the change: in DiGi Smart Monitor the actual cycle times from the machine signal and OEE split into availability, performance and quality, in DiGi Smart Control the measurements of characteristics and the Cpk trend before and after the change, and in DiGi Smart Trace the link between finished pallets, the raw material batch and the machine.
Five questions before you shorten the cycle
Before you change the settings, check:
- Do you know the flow in litres per minute on every circuit of the mould?
- Are you sure the flow in the mould channels is turbulent?
- Have you determined the gate freeze point by experiment?
- Do you measure the part temperature right after the mould opens?
- After shortening the cycle, have you checked the part dimensions on a CMM after 24 hours, once post-mould shrinkage shows?
Takeaway
An injection mould is a heat exchanger, not just a tool that gives the part its shape. A shorter cycle is a gain only when part measurements confirm it, including those taken a day later.
The part counts are a worked example (4-cavity mould, 25 s and 21 s cycle, no stops), not a result from a plant. Share of cooling in the cycle and the effect of limescale on cooling: Zink et al., “Modeling the effect of scale deposition on heat transfer in injection molding”, Scientific Reports 15 (2025). Turbulent flow threshold: Autodesk Moldflow documentation. The cover graphic is in Polish.
Over to you
How do you handle this in your plant? After shortening the cycle, do you measure the parts again after 24 hours, or is one measurement straight off the machine enough?
Actual cycle times and OEE in DiGi Smart MonitorRelated terms