Digital production control for metalworking
Tolerances in hundredths of a millimetre, dozens of orders a day and expensive machines. The dimension enters straight from the caliper and the micrometer, the control chart shows tool wear before a run of rejects, and OEE tells you why the CNC was down.
Sound familiar?
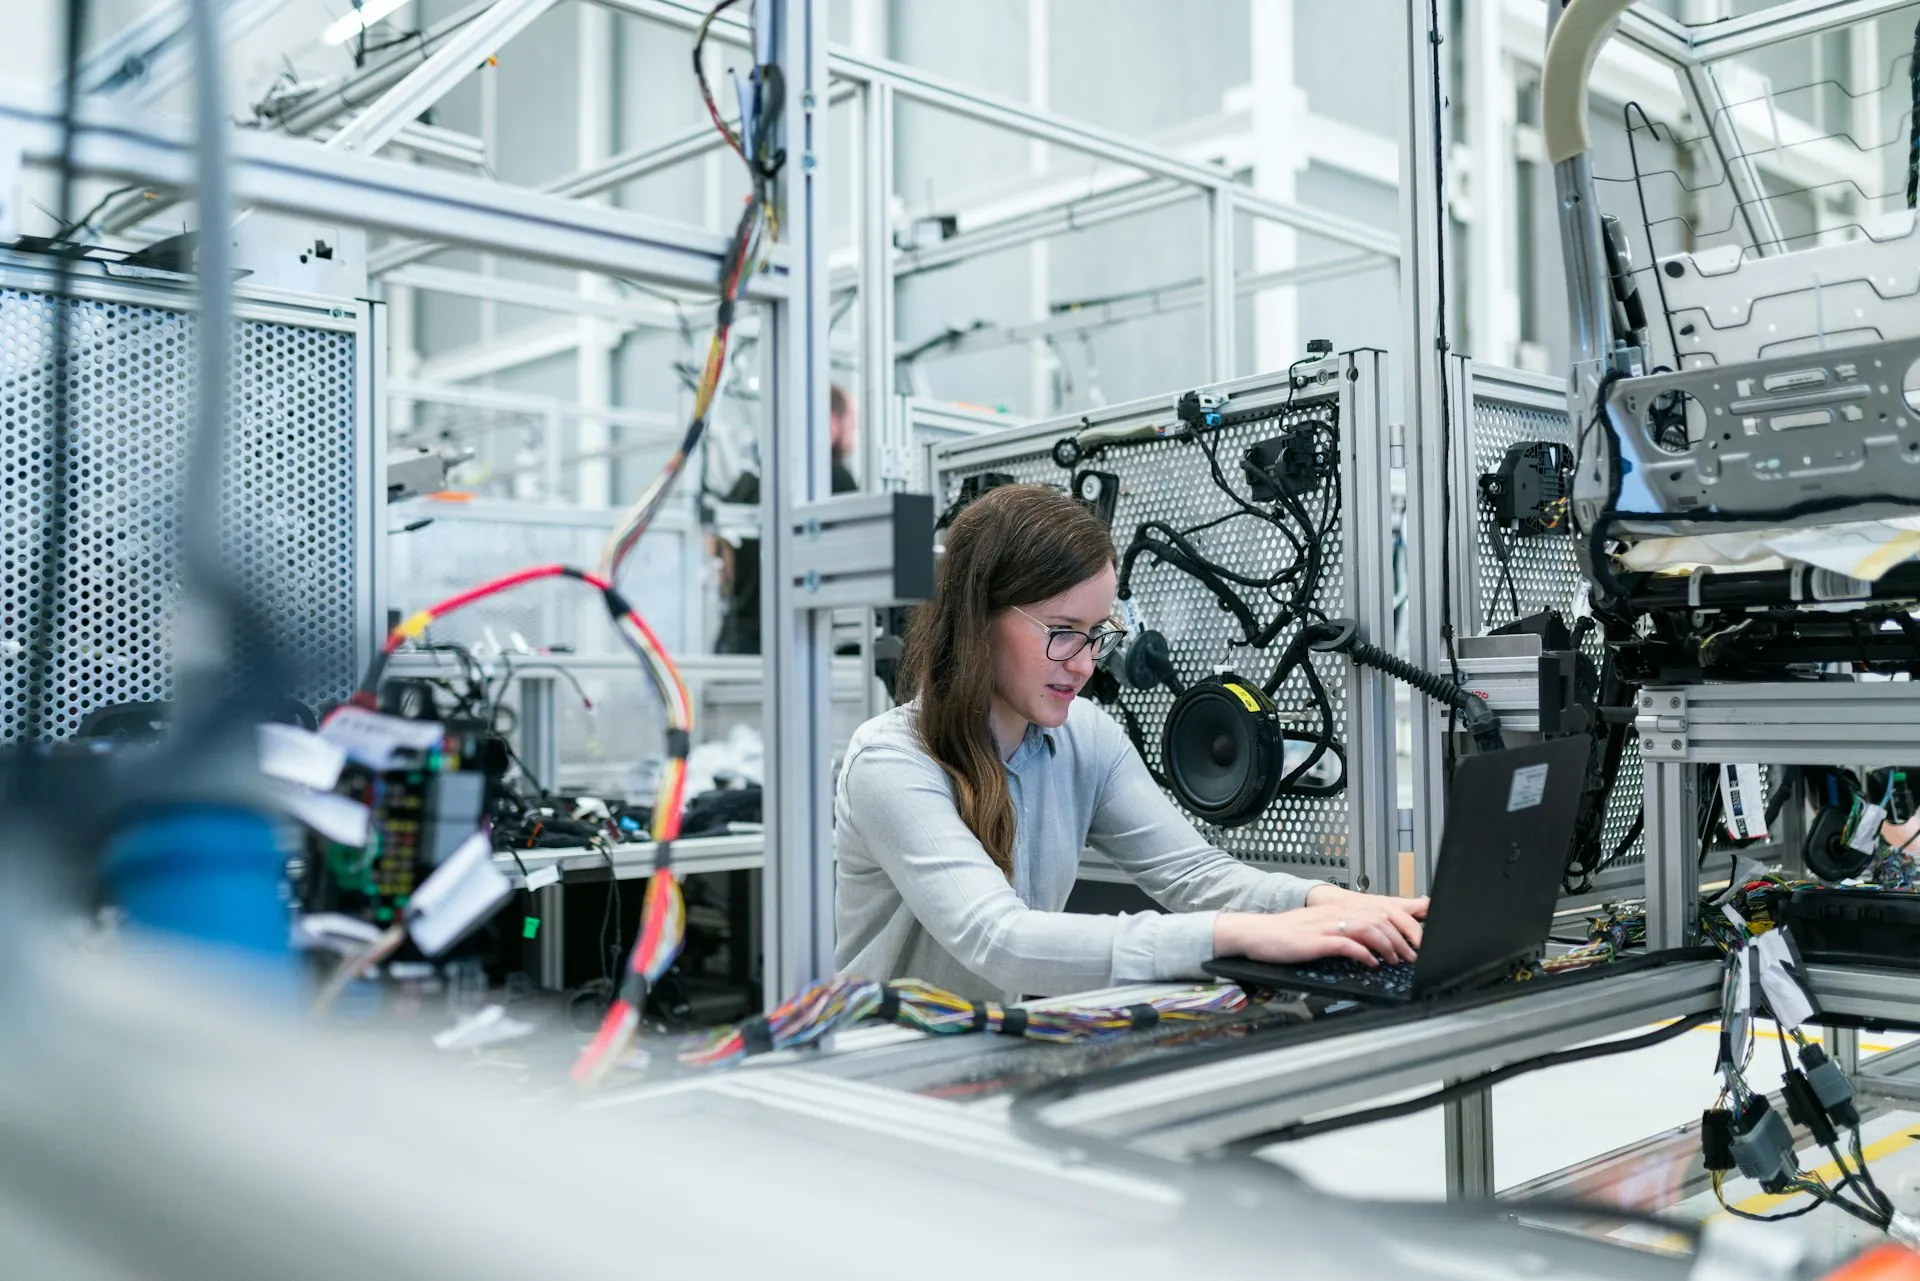
Tight tolerances, frequent changeovers and customers who require measurement reports. On the left the problem, on the right what the system does with it.
Tolerances in hundredths, measurements in a notebook
The caliper reading lands in a notebook, then in Excel. Retyping errors, no history and zero reaction at the moment of measurement.
A caliper and a micrometer with a Digimatic or Bluetooth output send the result at the press of a button, the roughness tester gives Ra. An immediate OK/NOK verdict, a history with the operator, the gauge and the piece number.
Tool wear shows up only after a run of rejects
The insert wears gradually, the dimension drifts toward the tolerance limit. Without a trend nobody sees it until rejects start.
The control chart shows the dimension drift over time and raises a trend rule alarm while measurements are still in tolerance. You replace the insert on a signal from the chart, not after a reject.
First piece after a changeover without inspection
A new order, a new program, new fixtures. The first article inspection depends on whether someone remembered.
First article inspection after a changeover in blocking mode: the tablet requires measuring all characteristics from the plan, and without approval the operator cannot start production.
The customer wants a measurement report with every delivery
A report, an SPC report or a certificate of conformity made by hand in Excel. Hours of work on every order.
You export the measurement history and the Cp and Cpk capability report per characteristic and order to PDF or XLSX. The report is ready the moment the inspection ends.
Expensive machines are down and nobody knows why
CNC, laser and press cost hundreds of thousands and still stand idle for part of the shift. No orders, material, changeover or breakdown? Everyone says something different.
The run signal from the gateway or a cycle sensor, the downtime reason from the operator at the moment of the event. A loss list in recoverable hours, breakdowns separate from organisation, MTBF and MTTR per machine.
Dozens of orders, a changeover between each
Different parts mean different programs, fixtures and tools. Nobody measures changeover time, so nobody shortens it.
A changeover has a start, an end and a plan on the timeline. The report shows the hours over plan per month, broken down by machine, part and operator.
One shift with DiGi
CNC lathe TK-03, flanged bushing, dimension Ø25 h7. Data from the demo company.
A new order on the lathe. The tablet requires a first article inspection: diameters from the micrometer, Ra from the roughness tester, the operator sees the balloon of the measured dimension on the drawing. Start after approval.
Ø24.99 mm with a tolerance of 25 h7. The result is OK, but the control chart shows six consecutive points going down. The signal: replace the insert before a reject.
The machine is down for 40 minutes. The operator picks "no material" from one dictionary of reasons. The loss goes to organisation, not breakdowns.
The measurement history of the order and the capability report to PDF. You send it in a minute, without retyping from cards.
Machine OEE for the day, a loss list ranked by hours, changeovers over plan. The report arrived by e-mail before the meeting.
Modules for this industry
Quality control and efficiency on one operator tablet. You add batch traceability when the customer asks about the material a part was made from.
DiGi Smart Control
Quality control
Dimensional inspection without retyping. A reading from the caliper, micrometer, indicator and roughness tester enters the system at the press of a button, and the control chart shows tool wear before rejects start.
Mitutoyo Digimatic, Sylvac Bluetooth, the SJ-210 roughness tester, KERN and Radwag scales. By cable, USB or Bluetooth, without drivers on the workstation.
Dimension drift on an I-MR or X-bar/R chart. The trend rule raises the alarm while measurements are still in tolerance.
After a changeover, in blocking mode. The operator sees the balloon of the measured dimension on the drawing and the instructions.
The measurement history and the capability report per order to PDF and XLSX. Without retyping from cards.
DiGi Smart Monitor
Production efficiency
How much does your CNC really run? The run signal from the gateway or a cycle sensor, downtime reasons from the operator and changeovers with a plan show where the time of expensive machines leaks.
Every machine with an OEE target and the gap to target. You see whether the problem is no orders, changeovers or breakdowns.
Start, end and plan on the timeline. Hours over plan per month, per machine, part and operator.
MTBF and MTTR from recorded breakdowns. Missing material, staff and orders in separate loss groups.
An old milling machine or a press gets a cycle sensor and a small input module. Without touching the machine program.
DiGi Smart Trace
Batch traceability
When the customer asks which heat a part was made from: a bar or sheet batch with the supplier's batch number and certificate, a scan at the workstation, genealogy from material to shipment.
Every delivery of bar, sheet or casting is a batch with a supplier and the supplier's batch number. You attach the certificate to the batch.
The operator scans the material label at the start of the order. The parts from this order inherit the material batch.
The customer asks about the material? You open the part batch and see the delivery, the supplier, the machine, the operator and the inspection results.
A bad material batch? The system shows every order and shipment it went into.
What your customers and auditors require
The system does not "grant compliance". It provides the records the auditor and the customer want to see, with a date, an operator and a gauge.
ISO 9001
A control plan per part, measurement history, gauge supervision with a calibration due date, a non-conformance and corrective action workflow.
Automotive and aerospace customers
First article inspection after a changeover, critical characteristics with SPC, an 8D report for a complaint, a Cp and Cpk capability report to PDF.
A measurement report with the delivery
The measurement history of the order with the operator, the gauge and the result, exported to PDF and XLSX without retyping.
Material certificates
A material batch with the supplier's batch number and document, linked to parts by a scan at the workstation.
Questions we hear in this industry
Yours is not here? Write or call, we reply within 24 hours.
Manufacturers that work with us

Let's talk about your production
We reply within 24 hours
Piotr will help you pick the solution that fits your production processes.
Phone: (+48) 668 211 736
Email: digismartcontrol@gmail.com